


A reflective sheeting sample can pass inspection while a later shipment creates problems: a different yellow, uneven nighttime brightness, harder liner removal or edges that lift during fabrication. For distributors and converters, the question is whether the next delivery will perform like the material already approved.
Reflective sheeting batch consistency means keeping optical, adhesive and processing properties within agreed limits across the roll, between rolls and between production lots. It requires a defined product specification, controlled manufacturing, comparable measurements and records connecting delivered rolls to their production history.
This guide explains the controls buyers should evaluate and manufacturers should establish. ABLAZE, the reflective material brand of Changzhou Zhenghe New Material Technology Co., Ltd., supplies reflective sheeting for signage, printing, traffic safety and vehicle identification. The appropriate inspection plan depends on the product construction, application and purchase specification.
What Should a Reflective Sheeting Batch Control Plan Include?
A useful control plan covers four connected areas: color, coefficient of retroreflection, adhesive performance and traceability. Thickness, liner behavior, surface quality and converting performance support those requirements.
Control area | What to define | Evidence to request |
|---|---|---|
Color | Daytime method, reference and tolerance; nighttime requirements where applicable | Measured results and controlled visual comparison |
Retroreflection | Required RA at specified angles, color and orientation | Results linked to identified sampling positions |
Adhesion | Substrate, application conditions, dwell and test procedure | Peel results and observed failure mode |
Processing | Thickness basis, liner release, printing and cutting conditions | Physical inspection and relevant production trial |
Traceability | Lot definition and parent-to-child roll identification | Roll labels, conversion records and shipment mapping |
These requirements should be agreed before production. Inspection becomes much less effective when buyer and supplier first discuss measurement conditions after a dispute.
What Counts as a Batch of Reflective Sheeting?
“Batch” and “lot” need a written definition. A purchase order, shipping container or production date does not necessarily identify one uniform manufacturing population.
A reflective product may involve separate face-film, optical-layer, adhesive-coating, lamination and converting operations. One finished roll can therefore have several relevant parent records. Conversely, one coated master roll may become many slit rolls sold under different customer labels.
A practical lot definition identifies the product code, color, construction revision, relevant manufacturing run and release status. Changes to critical raw materials or processing conditions should trigger a documented decision about whether a new lot designation is necessary.
For example, a hypothetical parent roll M-104 could become finished rolls M-104-01 through M-104-08. Each child remains linked to the parent, while its width, length and conversion details are recorded separately. These identifiers illustrate traceability; they are not an ABLAZE coding specification.
Good records distinguish a production lot from a delivery. A shipment containing three lots should identify all three and show which rolls belong to each.
Why Do Reflective Sheeting Properties Vary Between Batches?
Reflective sheeting is a layered optical and adhesive product. Variation can originate in incoming materials, manufacturing conditions, converting or storage.
Potential contributors include pigment dispersion, resin properties, face-film thickness, optical-element geometry, coating distribution, drying conditions and winding tension. The relevant variables differ between constructions; a control plan for glass-bead material should not simply be copied to microprismatic sheeting.
Variation also has a location. A narrow coating streak differs from a gradual shift across the web. A start-up section may behave differently from stable production, while a changeover can introduce a distinct transition within the run.
This is why one attractive sample or one reading from the center of a roll cannot describe the complete batch. Controls need to address variation across width, along length and over successive production runs.
The objective is measurable, repeatable performance within agreed limits. Claims of completely identical batches are less useful than a supplier explaining its tolerances, measurement methods and response to deviations.
What Does Manufacturing Control Look Like from Start to Finish?
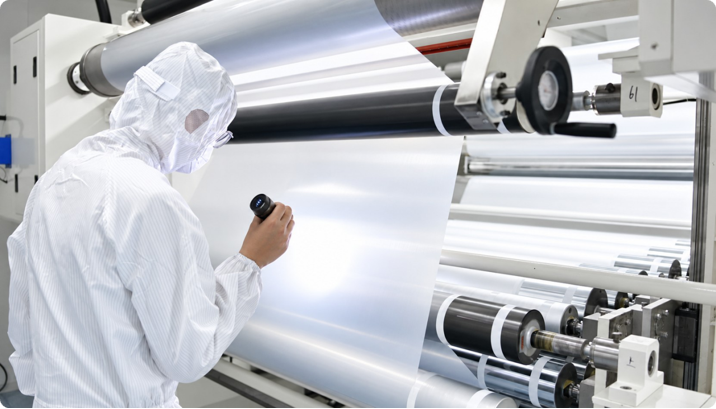
1. Verify incoming materials against approved requirements
Check the identity and status of materials before they enter production. Supplier documentation is useful, but critical characteristics may also require incoming verification. Link accepted material lots to their storage locations and intended production use.
The key question is whether an incoming change can affect finished performance. A resin substitution or liner revision should be assessed before consumption, even when the replacement appears commercially equivalent.
2. Approve the production setup
Use the correct formulation and process revision for the order. Confirm line settings, equipment readiness and measuring-device status. Evaluate start-up material before treating the run as stable production.
Record approval and the boundary between start-up waste and usable material. Without that boundary, later conversion can accidentally include sections that were never released.
3. Monitor the run and identify transitions
Record critical operating conditions at a frequency suited to the process. Where online monitoring is available, understand what it detects and what still needs offline testing.
Mark relevant interruptions, splices and adjustments against production time or material position. A record saying that an adjustment occurred is much more useful when it also identifies the potentially affected section.
4. Separate testing from shipment authorization
Finished material should have a clear status while required results are pending. Store or electronically identify material awaiting inspection so it cannot be mistaken for released stock.
The release decision should connect completed inspection to the defined lot. Testing selected specimens and authorizing an unidentified warehouse quantity leaves a gap in the control system.
5. Preserve identity through packing
Check finished-roll labels against conversion records and the packing list. Where an order contains multiple lots, identify the allocation rather than presenting the shipment as one undifferentiated quantity.
Retained samples should carry sufficient information to connect them to tested locations and delivered rolls. A shelf of unlabelled samples contributes little to a later investigation.
How Is Daytime Color Consistency Controlled?
Establish an approved reference and measurement method
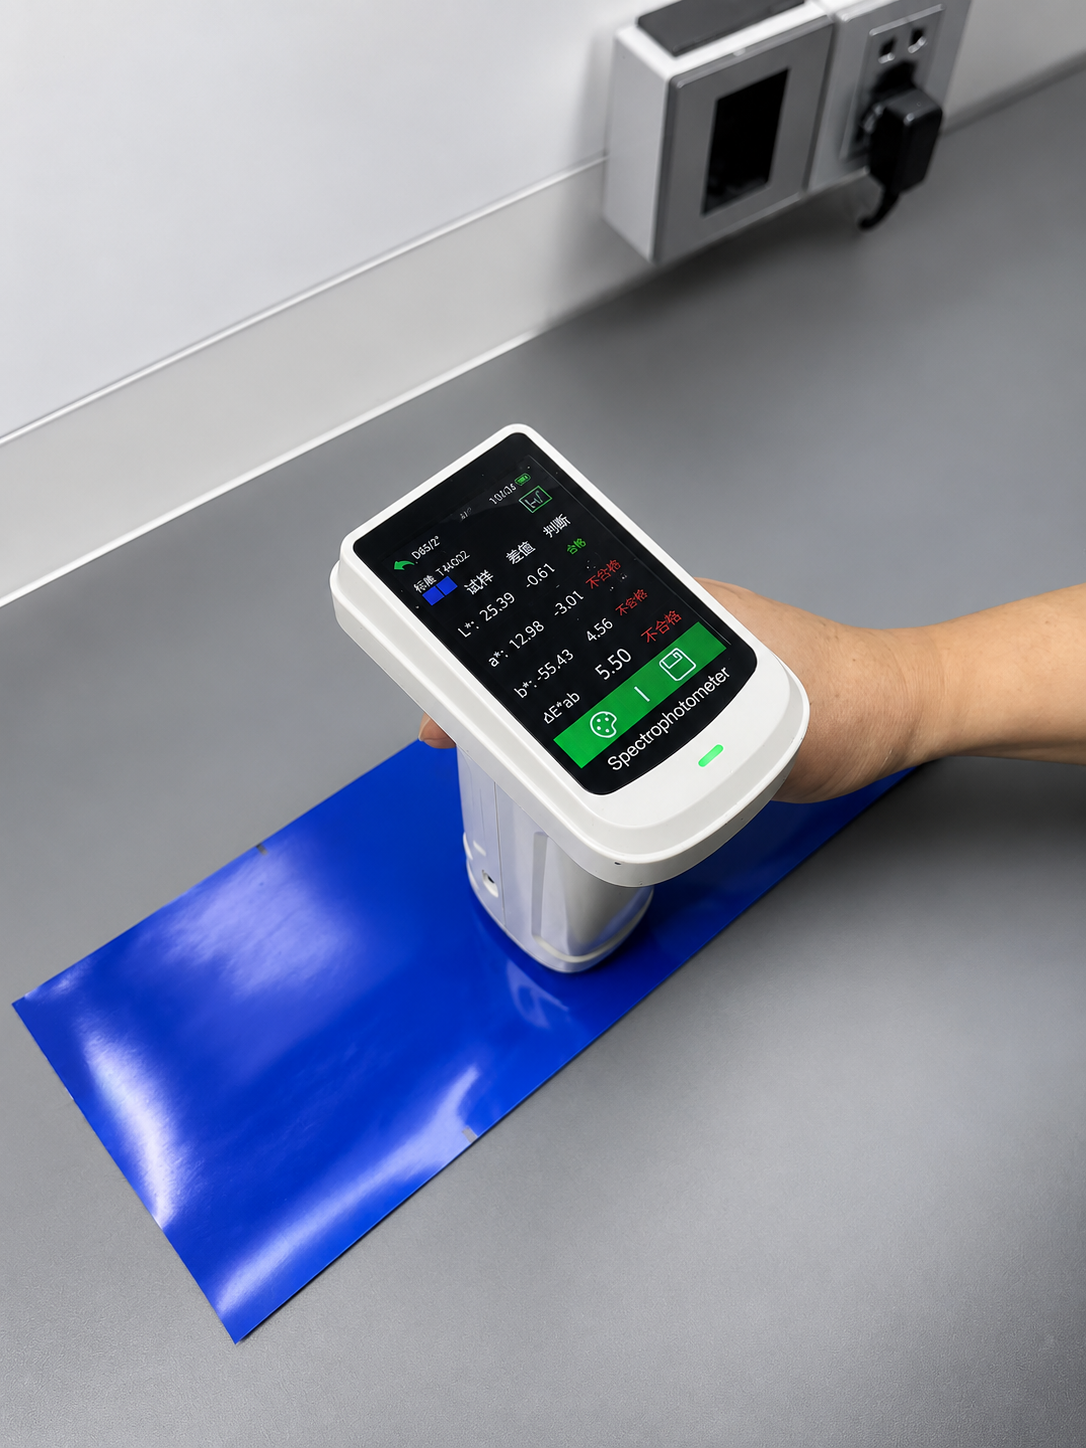
Start with a controlled reference that identifies the exact product and color. Record its approval date, construction revision and initial measurements. Protect physical reference samples from contamination, heat and light, and establish when they require review or replacement.
For regulated products, the governing specification may define acceptable chromaticity regions and luminance-factor requirements. Commercial graphics may also require a closer appearance match to an approved sample.
Those are different acceptance questions. Two yellow batches can both fall inside a permitted color region while looking different beside each other. State whether acceptance requires compliance, reference matching or both. Avery Dennison’s color-specification guidance explains the use of defined color regions for reflective materials.
Control the conditions behind the color number
A meaningful color record identifies the instrument, calibration status, measurement geometry, illuminant, observer and specimen preparation. Where relevant, record backing and UV settings, especially for fluorescent materials.
A color-difference result such as Delta E is incomplete without its formula and reference. There is no single universal Delta E limit suitable for all reflective sheeting colors, constructions and applications. Agree the method and tolerance for the actual project.
Use an instrument and procedure suitable for the material. Reflective and fluorescent surfaces can require particular measurement arrangements; a convenient general-purpose color meter should not automatically become the acceptance instrument.
Combine instrumental results with controlled visual matching
Inspect adjacent pieces under consistent lighting and viewing conditions. Check edge-to-center variation, streaks and differences between rolls intended for the same sign face or graphic.
Phone photographs help document a concern, but automatic exposure and white balance can conceal or exaggerate it. Instrumental measurements and retained specimens provide a stronger basis for deciding whether the material changed.
For its reflective graphic films, 3M’s production and color-matching bulletin calls for checking adjacent panels even within the same lot. This illustrates why lot identity supports, but does not replace, appearance verification.
Are Daytime Color, Nighttime Color and RA the Same?
No. Daytime color describes appearance under daytime measurement conditions; nighttime color describes the color of retroreflected light; RA measures the strength of the retroreflective response at a defined geometry.
A daytime color match does not establish nighttime color compliance. Likewise, a high RA result does not prove that the returned light has the correct chromaticity.
Where nighttime color is specified, use the required retroreflective measurement arrangement and source conditions. Do not substitute a daytime D65 result for a nighttime test using the illuminant prescribed by the applicable method.
This distinction is especially relevant to traffic signs, vehicle identification and adjacent reflective panels. Evaluate the finished visual arrangement as well as the individual material specimens. For any panel layout, follow the specific product’s fabrication instructions rather than assuming all reflective technologies behave identically.
How Do Manufacturers Control RA Consistency?
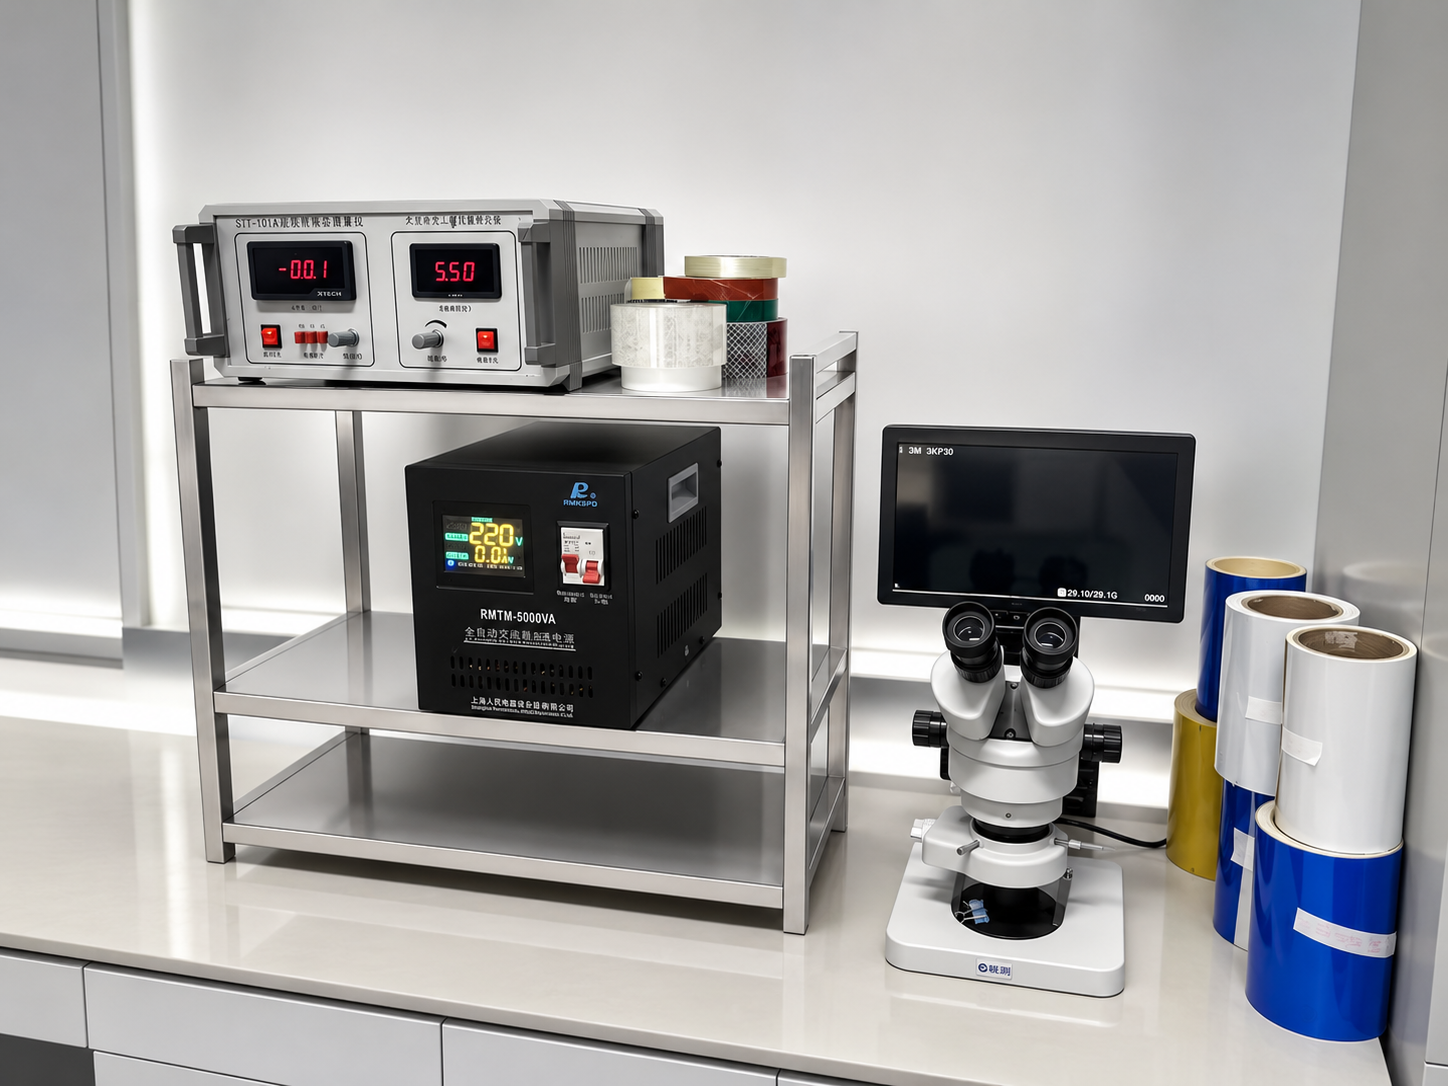
Compare like-for-like measurements
RA is the coefficient of retroreflection, commonly reported in cd/(lx·m²). It describes retroreflected luminous intensity relative to illuminance on the material and its area under specified geometry.
Every comparison needs the same observation angle, entrance geometry, specimen orientation, color and test method. A result measured at one geometry cannot replace a required result at another.
ASTM E810 addresses laboratory measurement of sheeting RA using coplanar geometry. Use the method required by the project; a portable instrument with limited geometry may support routine checks without covering the complete acceptance matrix.
Separate guaranteed minimum values from typical results. Also distinguish measurements on bare sheeting from those on printed, laminated or otherwise processed material.
Control the optical construction
For glass-bead constructions, relevant controls can include bead characteristics, distribution, embedment and the geometry of the surrounding optical layers. For microprismatic products, replication quality, prism geometry, sealing and protection of the optical structure can be important.
Manufacturers should identify which variables affect their particular construction and establish process settings and inspection points accordingly. Surface appearance alone cannot establish that the optical structure is performing correctly.
Any printing or laminate system introduced later needs separate evaluation. A consistent incoming roll can still produce inconsistent finished graphics if ink deposition or processing changes.
Check measurement reliability
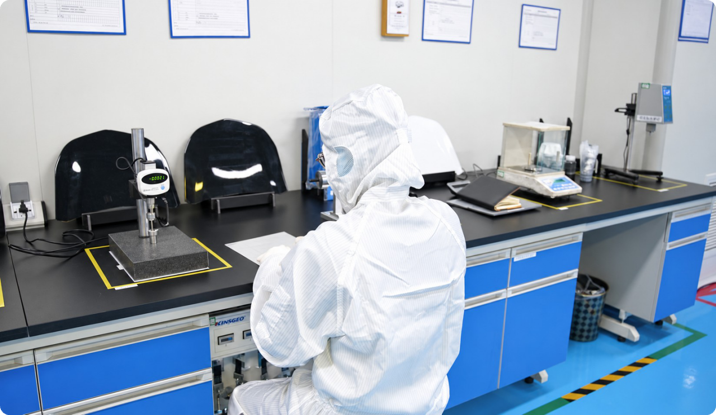
Use calibrated equipment, suitable reference standards and repeatable specimen positioning. Record the instrument identity and checks associated with the measurement session.
If buyer and supplier obtain different results, compare the method and specimen first. Orientation, instrument aperture, sampled area and calibration can all affect the comparison. For borderline results, agree how uncertainty and any referee testing will be handled before deciding acceptance.
NIST’s retroreflection work highlights the need for calibration traceability alongside standardized measurement procedures. Consistency of procedure alone does not establish instrument accuracy.
Passing the RA Minimum Does Not Prove Batch Uniformity
Consider a hypothetical requirement of 100 cd/(lx·m²) at one specified geometry. Four samples measure 112, 116, 145 and 149. Each exceeds that minimum, but their spread could still matter for adjacent panels.
These numbers are an example only, not a product classification or acceptance limit. Their purpose is to show why specification compliance and appearance consistency need separate evaluation.
Record individual measurements, their locations, the minimum and useful summary statistics. Averages help describe a population, but can hide a localized low result. Apply the acceptance statistic required by the governing method or contract.
Manufacturers can also track results over time. A gradual downward trend may justify process investigation even while measurements remain acceptable. Statistical control limits describe process behavior; specification limits define product acceptance. They should not be treated as interchangeable.
How Is Adhesive Consistency Controlled Between Lots?
Control formulation, coating and processing
An adhesive description such as “permanent acrylic” does not fully define performance. Relevant controls may include formulation revision, incoming material identity, solids content, viscosity under defined conditions, coating distribution and drying or curing conditions.
The appropriate variables depend on the adhesive system. For example, a solvent-based coating and a hot-melt system do not have identical process controls.
Coat weight also requires a clear basis. State whether a figure refers to wet coating, dry adhesive or total construction thickness. Two batches can have similar overall thickness while distributing material differently between layers.
Make adhesion tests comparable
A repeatable peel test identifies substrate preparation, specimen width, application pressure, conditioning, dwell time, peel angle, test speed and reporting units. Record whether failure occurs at the substrate, within the adhesive or elsewhere in the construction.
ASTM D3330/D3330M provides methods for pressure-sensitive tape peel testing and assessing uniformity. Confirm suitability for the sheeting construction; backing stiffness or extensibility can affect results. Peel numbers alone do not establish equivalent field performance between different products.
For application selection, see our reflective sheeting adhesive guide.
Verify the actual application
Routine checks on a controlled reference panel help reveal manufacturing drift. Trials on the customer’s real substrate answer a different question: whether the material suits the application.
Keep these evaluations connected. An unchanged adhesive may behave differently after a change in panel coating, cleaning chemistry or installation temperature. Preserve a record of those conditions so a processing change is not misdiagnosed as a material defect.
Why Do Thickness, Liner Release and Converting Matter?
A batch can meet optical requirements yet slow production through difficult weeding, liner separation, curl or inconsistent feeding. Processing properties therefore deserve written controls alongside RA and color.
Define whether thickness includes adhesive, liner or both. Measure at identified positions using a suitable procedure, and avoid comparing values reported on different construction bases.
For release liners, specify the relevant material, weight and release behavior. A 150 gsm liner is not automatically interchangeable with another 150 gsm liner. Silicone treatment, moisture condition and stiffness can influence handling. A planned change from 150 gsm to 120 gsm should be reviewed as a product change.
Slitting and winding introduce their own risks. Check slit width, edge quality, core condition, telescoping, wrinkles and roll identification. Maintain the connection between parent and child rolls after cutting or repacking.
For printable material, keep a repeatable test pattern and processing settings. Where relevant, evaluate ink adhesion, curing, cutting and the finished reflective appearance using the intended production system.
What Is a Practical Sampling Plan for Reflective Sheeting?
A useful sampling plan defines the lot, selected rolls, sampling locations, tests, acceptance rules and response to failure. Sample quantity should follow the governing specification or an agreed plan reflecting order size and risk.
The following is a planning framework, not a universal sampling standard:
Sampling dimension | Suggested coverage | What it helps reveal |
|---|---|---|
Across the web | Defined positions near both edges and at the center | Cross-web drift and coating differences |
Along production | Recorded beginning, intermediate and end locations | Start-up, gradual drift and end effects |
Between rolls | Selected finished rolls throughout the lot | Conversion variation and mixed material |
Between lots | Comparable records from repeat deliveries | Longer-term shifts |
Around changes | Additional checks near relevant changeovers | Transition-related defects |
The manufacturer can sample material during production that is inaccessible once wound. A buyer inspecting delivered rolls should understand what head samples can establish and what production records must cover.
Agree on destructive sampling, accessible locations and responsibility for inspection waste. Increasing the number of readings does not correct a poorly defined lot or biased sample selection.
If an AQL plan is specified, identify the governing standard, inspection level and defect categories. AQL is a sampling parameter; it does not authorize shipment of known defective material.
How Should Roll-to-Raw-Material Traceability Work?
Traceability should answer two questions: what produced this roll, and where did related material go? A batch number is useful only when records can answer both.
A workable record chain connects incoming material lots to manufacturing runs, master rolls, inspection results, finished rolls and shipment lines. Where multiple coating or lamination stages are involved, preserve the relationships between those stages.
The buyer-facing label can remain simple. Product code, color, lot number, unique roll identity and dimensions may be sufficient when the underlying production history remains retrievable. Private-label artwork should preserve the original traceability link.
For slit rolls, record parent identity and, where practical, the originating width position and length section. This can help distinguish a localized defect from a problem affecting the entire parent roll.
Consider another hypothetical example: one slit roll shows an RA streak near an edge. Parent and position records can guide targeted inspection of related rolls. Without that information, a much broader shipment may require investigation.
Barcode or QR systems can simplify retrieval, but printing a code is not proof of traceability. Test whether staff can retrieve the associated manufacturing, inspection and shipment records from an actual delivered roll identifier.
Which Documents Demonstrate Batch Consistency?
Different documents answer different questions. Buyers should request an evidence package that matches their application and purchasing risk.
Document | Question it answers | Limitation |
|---|---|---|
Technical data sheet | What is this product intended to deliver? | Usually describes the product rather than a specific shipment |
Batch inspection report or CoA | What was tested on this identified lot? | Its usefulness depends on sampling and reported conditions |
Certificate of conformity | What conformity statement is being made? | May contain no measured results |
Independent test report | What did the laboratory measure on submitted specimens? | Does not automatically cover later production |
Roll and packing records | Which material was delivered? | Identification alone does not demonstrate performance |
A meaningful batch report identifies the product revision, lot, sampled rolls, specimen locations, test methods, conditions, results and release decision. Generic pass statements are less informative than results traceable to the ordered material.
Start with our guide to reading a reflective sheeting technical data sheet when aligning document terminology.
What Should Happen When a Batch Drifts or a Material Changes?
Separate suspected material from released stock and preserve its identity. Define the potentially affected production range using process history, sampling locations and related roll records.
First confirm the measurement system. Then investigate relevant materials, settings, changeovers and downstream processing. Retesting should follow a documented rule; repeatedly sampling until a favorable number appears does not resolve the original finding.
Disposition may involve rejection, rework where feasible, further evaluation or a specifically authorized concession. Document who decided and which material the decision covers. Verify corrective action on later production and retain the supporting evidence.
Change control should address intentional modifications as well. Depending on the project, a new pigment source, adhesive system, face film, liner or manufacturing route may require notification, testing or renewed approval.
An updated label cannot substitute for evaluating a changed construction. Keep the approved product revision aligned across samples, purchase orders, technical information and delivered rolls.
How Should Buyers Investigate a Difference After Delivery?
Begin by holding the affected rolls and recording their labels, locations and observed symptoms. Preserve unused material from the questioned section and a comparison specimen from previously accepted stock.
Suppose a converter reports that a new shipment weeds badly while the previous one ran smoothly. First compare product and liner identities, storage conditions and conditioning time. Then check blade wear, cutting depth, speed and the actual cut pattern. Run both specimens under the same controlled settings.
If the difference persists, compare liner release and other relevant measurements with the supplier. This sequence creates evidence that can distinguish a material change from equipment or environmental effects without assuming the cause in advance.
For optical complaints, preserve specimen orientation and compare the same color at the same geometry. Send the supplier individual readings, instrument details and sampling positions, rather than only a photograph of a bright and dark patch.
An agreed investigation package makes resolution faster: order reference, roll identities, issue description, specimen location, test conditions, representative samples and records of processing already performed. Keep unaffected stock identifiable while the investigation establishes the true scope.
How Can Buyers Specify Consistency Before Ordering?
Translate expectations into a purchase specification. “Same quality as last time” leaves too much undefined, especially when multiple product versions share a commercial name.
Specify the exact model, color, construction revision, dimensions, thickness basis, adhesive and liner. Identify the approved reference and required standard edition where applicable.
For traffic-control projects, ASTM D4956 is a relevant sheeting specification when required by the contract. Its scope excludes inks, overlays and other imaging methods. Qualification of the base material therefore should not be presented as automatic approval of every finished printed construction.
Then define color tolerances, the RA measurement matrix, adhesion conditions, processing trials, sampling rules, traceability and required documents. For appearance-sensitive assemblies, address lot allocation and panel-matching procedures.
An example purchasing clause is:
Supply the approved product construction and revision. Identify production lots and finished rolls on labels and shipment records. Evaluate sampled material using the agreed color, retroreflection, adhesion and physical-property methods. Obtain written approval for changes requiring customer qualification before shipment.
This is a starting point; project-specific tolerances and responsibilities still need to be completed. For qualification planning, use our guide to testing reflective sheeting before a bulk order.
Discuss Your Batch Requirements with ABLAZE
Changzhou Zhenghe New Material Technology Co., Ltd. supplies ABLAZE reflective materials for different converting and end-use requirements. Begin with the application, destination market, substrate, processing method, required color, order quantity and governing specification.
For rigid-sign projects, review our high-intensity prismatic reflective sheeting. Printing businesses can explore ABLAZE printable PVC reflective vinyl, while plate manufacturers can review reflective film for license plates.
Before confirming a repeat order, ask us to agree the relevant product specification, reference sample, inspection scope and documentation requirements. Any special tolerances, reporting formats or traceability arrangements should be confirmed for the selected product and order.
Frequently Asked Questions About Reflective Sheeting Batch Consistency
Can two compliant batches look different?
Yes. Meeting a minimum RA value or a permitted color region does not necessarily ensure a close appearance match. Adjacent-panel applications may need additional matching requirements.
Does using one batch guarantee uniform panels?
No. Within-roll variation, orientation and subsequent processing can still affect appearance. Check adjacent pieces and follow the specific product’s fabrication guidance.
What is an acceptable RA difference between batches?
There is no universal percentage for every product. Define required minima and any additional uniformity criterion using the relevant color, geometry, application and measurement capability.
Is a batch certificate enough to accept a shipment?
It is useful when it identifies the delivered lot and suitable tests. Check its relationship to roll labels, sampling and actual results, alongside the purchase requirements.
Can a flashlight replace an RA test?
No. A controlled flashlight comparison can reveal visible differences, but it cannot provide calibrated RA values or establish compliance with a numerical requirement.
How long should manufacturers retain batch samples?
Set retention periods according to product life, contractual obligations, storage stability and investigation needs. Keep measured baseline data because physical specimens can change during storage.
Does a consistent batch guarantee outdoor durability?
No. Batch checks verify defined characteristics. Outdoor performance also depends on the qualified construction, exposure, processing and installation. Long-term qualification and routine release testing serve different purposes.
RELATED NEWS

Sun, Sand and a 50°C Container: Getting Reflective Sheeting Through a Hot Climate
In hot regions, reflective sheeting can start ageing before it reaches the sign shop. UV, heat, dust and humidity each attack a different part of the product, and each needs its own defence.Picture a distributor in a hot coastal city who receives a container of prismatic sheeting in midsummer. It si
